Containerized engineering, no more logistical compromises.
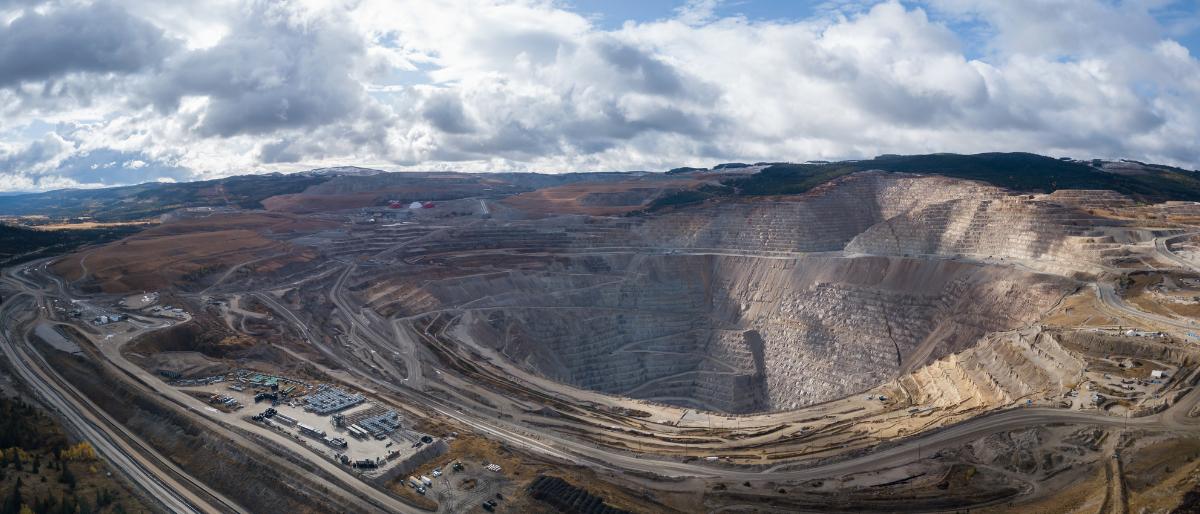
On a mining site in the Far North, a logging camp, or a remote power station, failure is not an option — and traditional jobsite logistics become a monumental challenge.
Our engineering division designs mobile water treatment plants that are fully pre-assembled and integrated inside modified shipping containers — plug-and-play upon arrival at your site.
To guarantee absolute thermal integrity against harsh climates, every unit is heavily insulated and heated. Internal piping in Schedule 80 PVC and 316 stainless steel comes pre-tested under pressure at the factory.
High-capacity Altum Series reverse osmosis systems, multi-media filters for high-turbidity water, Viqua PRO or Aquafine UV disinfection systems — every container incorporates our custom industrial PLCs.
This embedded intelligence allows the plant to self-adjust automatically to incoming water variations. Real-time monitoring via Ethernet, BACnet, and Modbus — your operators and our experts monitor operations together, without requiring a constant human presence on site.
Factory pre-assembled and tested shipping container
Thermal insulation & Arctic-grade heating
Atmospher PLC & industrial telemetry
Ethernet, BACnet & Modbus monitoring
Built for extremes
From −40°C to +55°C, your operations never stop
Our shipping containers are engineered to operate without interruption in the most hostile environments in Canada and internationally.
Arctic conditions
Built for extreme cold
Our containers are heavily insulated, ventilated, and heated to operate continuously in the most hostile environments of the Canadian Far North.
Reinforced insulation — treated walls and floor
Integrated heating — internal temperature maintained
Protected piping — antifreeze and heat tracing
Try it ↓
ColdHot
Click to toggle
−40°C
Minimum operating temperature
Tested and certified
Canadian Far North conditions
Our methodology
4 steps to deliver a turnkey treatment plant, anywhere in the country
From the pre-assembled shipping container to remote monitoring — every remote site becomes a controlled operation, with no building to construct and no specialist to house on location.
Step01
Container pre-assembly
Full integration of a treatment plant into a modified shipping container. High-capacity Altum Series reverse osmosis train, multimedia filters for high-turbidity water, UV disinfection from Viqua PRO Series or Aquafine. Internal PVC 80 and 316 stainless steel piping, pressure-tested at the factory before shipment.
Step02
Extreme thermal insulation
To guarantee absolute thermal integrity in the harsh climates of the Far North, each container is heavily insulated and heated. Architecture designed for continuous operation in extreme temperatures — no risk of pipe freeze, no winter production downtime.
Step03
Embedded intelligence
Programming of our custom-built Atmospher industrial PLCs. The station automatically adjusts to variations in incoming water quality — without requiring the constant on-site presence of a technician at your remote location.
Step04
Off-grid delivery
Container delivered ready to operate. Real-time monitoring via Ethernet, BACnet, and Modbus — flow rates, alarms, and conductivity accessible to both your camp operators and our experts. Zero on-site construction, zero specialized technician housing required in the field.
Secure the water supply for your remote sites.
Mining camps, logging operations, remote power stations — request a consultation for the sizing and manufacturing of your custom containerized treatment plant, delivered ready to operate.